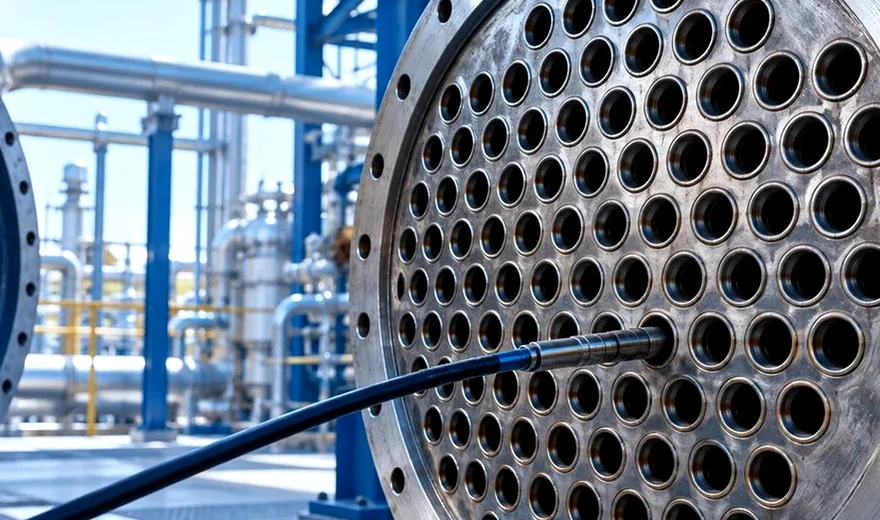
Tube bundles
Discuss exchanger tube material, dimensions and access.
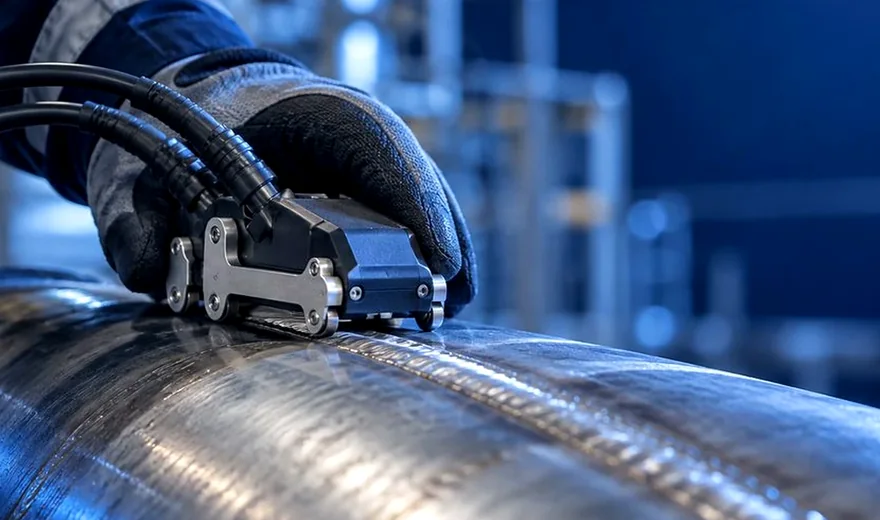
Explore →A weld surface programme should define the weld material, geometry and target flaw, then demonstrate that the selected probe and calibration can examine the required zones. Weld cap shape, toes, roughness, coating and magnetic properties can affect lift-off and signal interpretation. ASTM E3052 addresses carbon steel weld examination using ECA; ISO 17643 covers weld eddy current testing by complex-plane analysis. Neither citation alone establishes a project procedure.
Request a proposal Explore servicesInspection scope, suitable probe design, reference standards and reporting requirements should be determined for the actual asset. Where feasibility is uncertain, send the drawings and inspection objective for review.
Surface and near-surface indication planning.
Explore application →
Bundle survey and localised tube indications.
Explore application →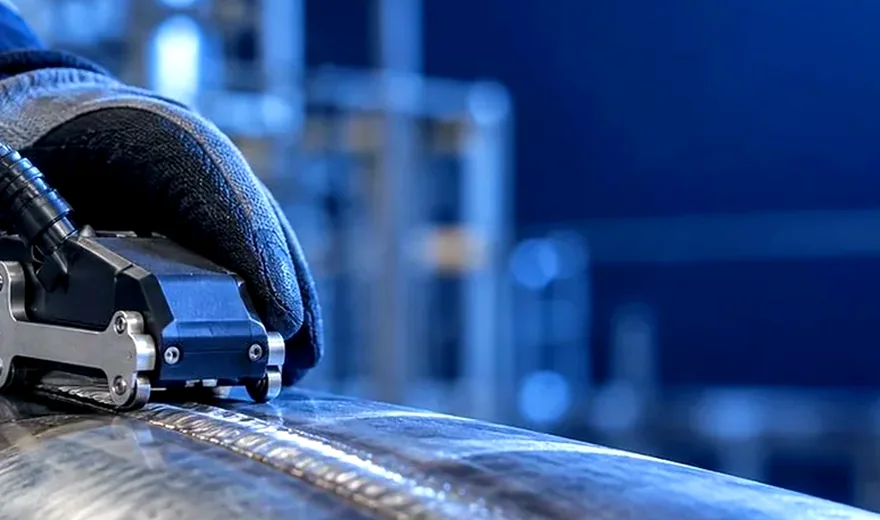
Plate and accessible detail inspection.
Explore application →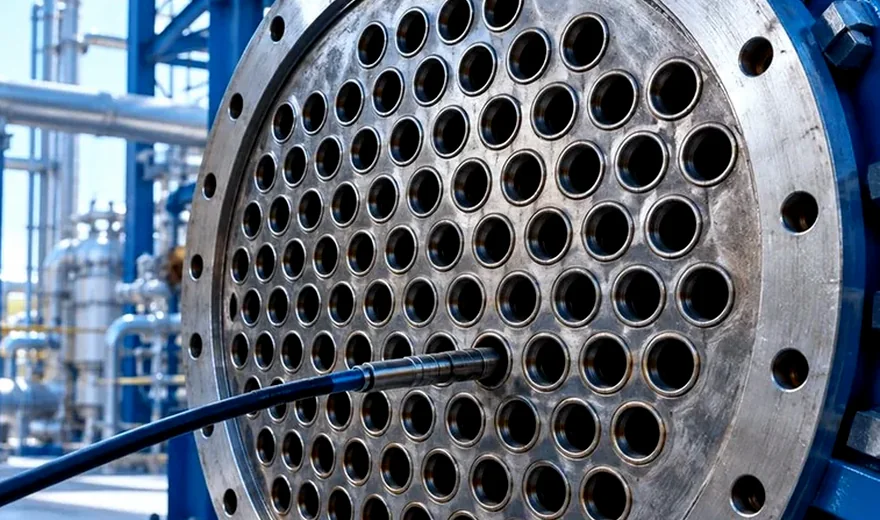
Expansion and support-region concerns.
Explore application →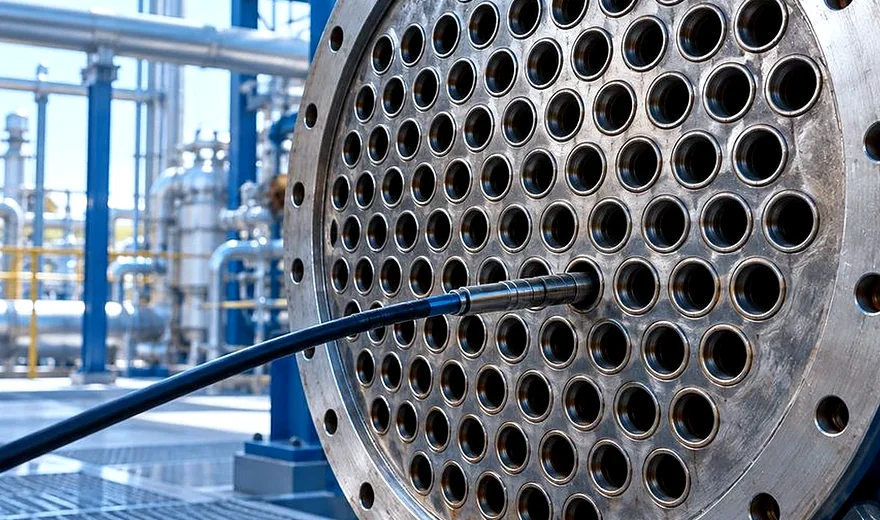
Weld maps, material, thickness, profile, coating, expected indication and applicable edition.
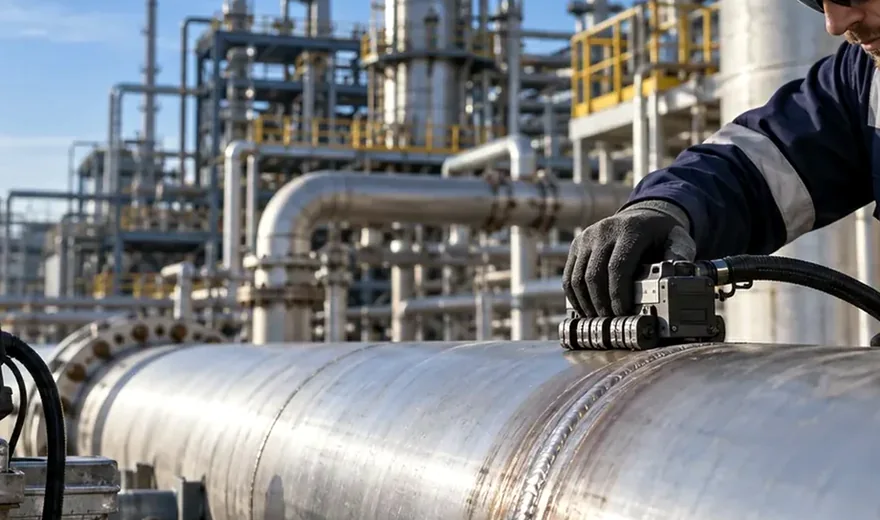
Probe coverage, scanning direction, calibration pieces, sensitivity and reporting.
Relevant signals are interpreted against the agreed procedure and acceptance basis.
The inspection route is selected for the actual material, geometry, access and damage objective. Standards are applied only when they are relevant to the agreed project procedure.
Method selection starts with material conductivity and magnetic properties, component geometry, surface condition, access, expected flaw orientation and the decision the inspection must support. Probe arrangement, frequency, reference standards, calibration, scanning pattern and reporting are then defined for the actual component.
Examples can include ASTM E3052-21 for examination of carbon steel welds using ECA, ISO 15549:2019 for general eddy current testing principles, and ISO 17643:2015 for eddy current testing of welds by complex-plane analysis. ASTM E243-24 addresses copper and copper-alloy tube ECT using encircling coils and is not an ECA-specific array procedure. The applicable edition, calibration approach and acceptance criteria should be agreed in the project procedure.
Contact IAIS with the component details and required schedule. Inspection capability and commercial terms are confirmed after scope review.
Discuss your inspection